Pure Copper
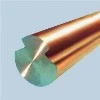
Pure copper contact wires typically have a tensile strength of 350 MPa and an electrical conductivity of 97.5% IACS. After undergoing a softening process, their tensile strength drops to only 60% of the original value. These wires are produced by drawing oxygen-free copper rods, and their mechanical strength is derived solely from work hardening.
While they offer excellent electrical conductivity and good corrosion resistance, they suffer from several drawbacks: 1. Inconsistent hardening between the surface and the interior; although strength increases with the degree of cold working, the material becomes more prone to softening, leading to a significant loss of strength. 2. Low overall strength, which increases the risk of wire breakage and failures in the pantograph-catenary system. 3. Low softening temperature and poor heat resistance. 4. Poor wear resistance; as the power of electric traction locomotives increases, electrical wear accelerates, significantly shortening the service life of the wire. Consequently, pure copper contact wires are unsuitable for high-speed, high-traffic, or heavy-haul lines and are generally restricted to low-speed railway applications.
Copper Alloys
Alloying can significantly improve the heat resistance, softening temperature, and mechanical strength of pure copper contact wires. By incorporating small, precise amounts of various alloying elements-a strategy known as "multi-element micro-alloying"-the impact on electrical conductivity is minimized, allowing the wires to meet the stringent requirements of high-speed electrified railways. Common alloying elements used in the development of these wires include Ag, Cd, Cr, Zr, Sn, Mg, and Re. Copper alloy contact wires offer high strength at elevated temperatures and superior wear resistance, with only a marginal reduction in electrical conductivity. Due to this excellent balance of properties, they have become the dominant choice for catenary systems on electrified railways. To ensure safe and reliable transport and power supply, reduce maintenance needs, and optimize technical and economic outcomes, the Ministry of Railways has advocated for the widespread adoption of copper alloy contact wires on heavy-haul lines, busy main lines, high-speed routes, and during major line-renewal projects. Globally, high-speed electrified railways almost exclusively utilize copper alloy contact wires.
1. Silver-Copper Alloy Contact Wires
This category includes silver-copper alloys and copper-tin-silver alloys. The performance of silver-copper and copper-tin-silver contact wires produced in my country is comparable to that of their international counterparts. However, further improvements in the straightness of these wires are required to reduce the rate of contact loss (arcing) between the pantograph and the contact wire. Research on silver-copper alloy contact wires has primarily focused on the effects of adding a second-or even a third-alloying element on the wire's performance. The addition of trace amounts of rare-earth elements can enhance the strength, hardness, and heat resistance of silver-copper contact wires; the tensile strength can reach 470 MPa-an increase of 73 MPa over standard silver-copper wires-with minimal impact on electrical conductivity.
2. Copper-Tin Alloy Contact Wires
Most high-speed railway systems worldwide utilize contact wires primarily made from copper-tin or copper-magnesium alloys. Compared to other types, copper-tin alloy contact wires offer a simpler manufacturing process, higher production yields, and a relatively lower cost.
3. Copper-Chromium-Zirconium (Cu-Cr-Zr) Alloy Contact Wires
Cu-Cr-Zr contact wires exhibit superior mechanical properties. Most notably, their recrystallization temperature is significantly higher than that of pure copper, and they maintain high strength at elevated temperatures. Chromium (Cr) has very limited solid solubility in the copper matrix, which minimizes the adverse effects of solute atoms on electrical conductivity. Zirconium (Zr) possesses a high melting point and excellent corrosion resistance. Furthermore, both chromium and zirconium can form oxides that facilitate grain refinement within the copper matrix, thereby enhancing the tensile strength of the contact wire. The addition of trace amounts of magnesium (Mg) and silicon (Si) to the Cu-Cr-Zr alloy creates multi-component strengthening phases, which significantly improve high-temperature resistance. Additionally, the hard chromium-based particles greatly enhance the wear resistance of the contact wire, with tensile strength reaching 555.5 MPa and electrical conductivity achieving 78.8% IACS.
4. Copper-Magnesium Alloy Contact Wires
Copper-magnesium alloy contact wires are widely used in Germany and Spain. These alloys can achieve a tensile strength of 500 MPa. For a given alloy content, copper-magnesium contact wires demonstrate superior wear resistance and better high-temperature performance compared to copper-tin contact wires. However, the manufacturing process for copper-magnesium contact wires is more complex and involves a greater number of production steps than that of copper-tin wires. Higher magnesium content increases processing difficulty; specifically, when the magnesium content exceeds 0.7%, the contact wire is prone to fracturing during the manufacturing process. Due to the complex production techniques involved, the output of copper-magnesium contact wires is relatively low. High-strength copper-magnesium alloy contact wires can withstand significant suspension tension. Their small cross-sectional area helps increase the propagation velocity of mechanical waves along the wire, thereby facilitating higher train operating speeds. Copper-magnesium alloy wires also exhibit excellent heat resistance and wear resistance. Although their electrical conductivity is relatively low, they can be paired with copper-alloy messenger wires, resulting in a simpler manufacturing process and lower costs. Through continuous casting and continuous extrusion, the as-cast grains of the oxygen-free copper-magnesium alloy rod are broken down; subsequent recrystallization-driven by deformation heat-produces a rod blank with a fine-grained microstructure. This blank then undergoes cold working to create a high-strength copper-magnesium alloy contact wire characterized by ultra-fine grain strengthening. This production process is simple and reliable, with output and quality that fully meet the requirements of existing high-speed electrified railways.
Steel-Aluminum Types
Steel-aluminum contact wires are produced by bonding steel and aluminum together through mechanical pressure processing. Issues associated with these wires include: 1) low bond strength, which can lead to separation; 2) electrochemical corrosion resulting from the difference in electrochemical potential between the steel and aluminum phases; 3) poor resistance to salt spray and atmospheric corrosion; and 4) a high number of joints, which increases the risk of fracture and reduces the reliability of the overhead contact system. Because aluminum has lower electrical conductivity, a larger cross-sectional area is required to ensure sufficient current-carrying capacity; however, this increases the load on the wire from wind, ice, and snow. The CGLN-250 aluminum-clad steel contact wire (produced in my country) and the TA-196 aluminum-clad steel contact wire (developed in Japan) both possess relatively low tensile strength and electrical conductivity. Nevertheless, due to their large cross-sectional areas, they are capable of meeting the breaking-force requirements for both quasi-high-speed and high-speed overhead contact systems.
Copper-Clad Steel Types
The copper-to-steel ratio in copper-clad steel contact wires can vary between 20% and 85%, allowing for the production of wires with various combinations of electrical conductivity and mechanical strength. The research and development of high-quality, domestically produced copper-clad steel contact wires is of great significance. Common production methods for copper-clad steel wire include the casting-hot-pressing process, electroplating, the dip-coating upward-drawing process, and continuous extrusion cladding. Among these, continuous extrusion cladding stands out as an ideal production process: it requires lower equipment investment, offers high productivity, ensures a uniform copper cladding thickness-free from exposed steel or weld seams-and delivers superior internal quality, high electrical conductivity, and low production costs.